Press Brake Machine Vendor Selection Guide for Precision Fabrication
2026-09-18
Choosing the right press brake vendor can make or break your precision fabrication line. Too many shops settle for machines that promise accuracy but deliver vibration, inconsistent bends, and costly rework. This guide cuts through the noise, focusing on what actually matters—repeatability, tooling compatibility, and support that doesn’t disappear after installation. Whether you’re upgrading a single machine or planning a full production cell, the wrong decision will quietly eat your margins. Before you sign anything, ask the questions most buyers skip. And if you’re tired of generic answers, explore HUNSONE for a different approach to bending precision.
How Close Is Close Enough for Your Bend Tolerances?
When sheet metal bends, every degree and every fraction of a millimeter matters. But chasing tighter tolerances than your process can hold doesn’t improve quality; it just drives up scrap and setup time. A bend tolerance that looks good on a drawing but can’t be repeated on the floor is worse than a looser one that holds every time.
Start with the capabilities of your press brake, tooling, and material. Air bending typically holds ±0.5° to ±1° on angle, while coining can get you closer, but at higher tonnage and tool wear. For linear dimensions, expect variation from material thickness, grain direction, and springback. If your drawing calls for ±0.1 mm on a bend line, ask whether the part actually needs that precision or if it’s just a default from the CAD template.
A practical approach is to separate functional tolerances from everything else. Dimensions that locate mating features or affect assembly should be tight, but a bend that only clears a cable or a finger can be loose. Review the tolerance stack across multiple bends; a series of ±0.5° angles can add up to a 1 mm positional shift at the far end. Decide what’s truly critical, then set tolerances your shop can hit without constant adjustment.
The Frame Tells You More Than Any Spec Sheet Will
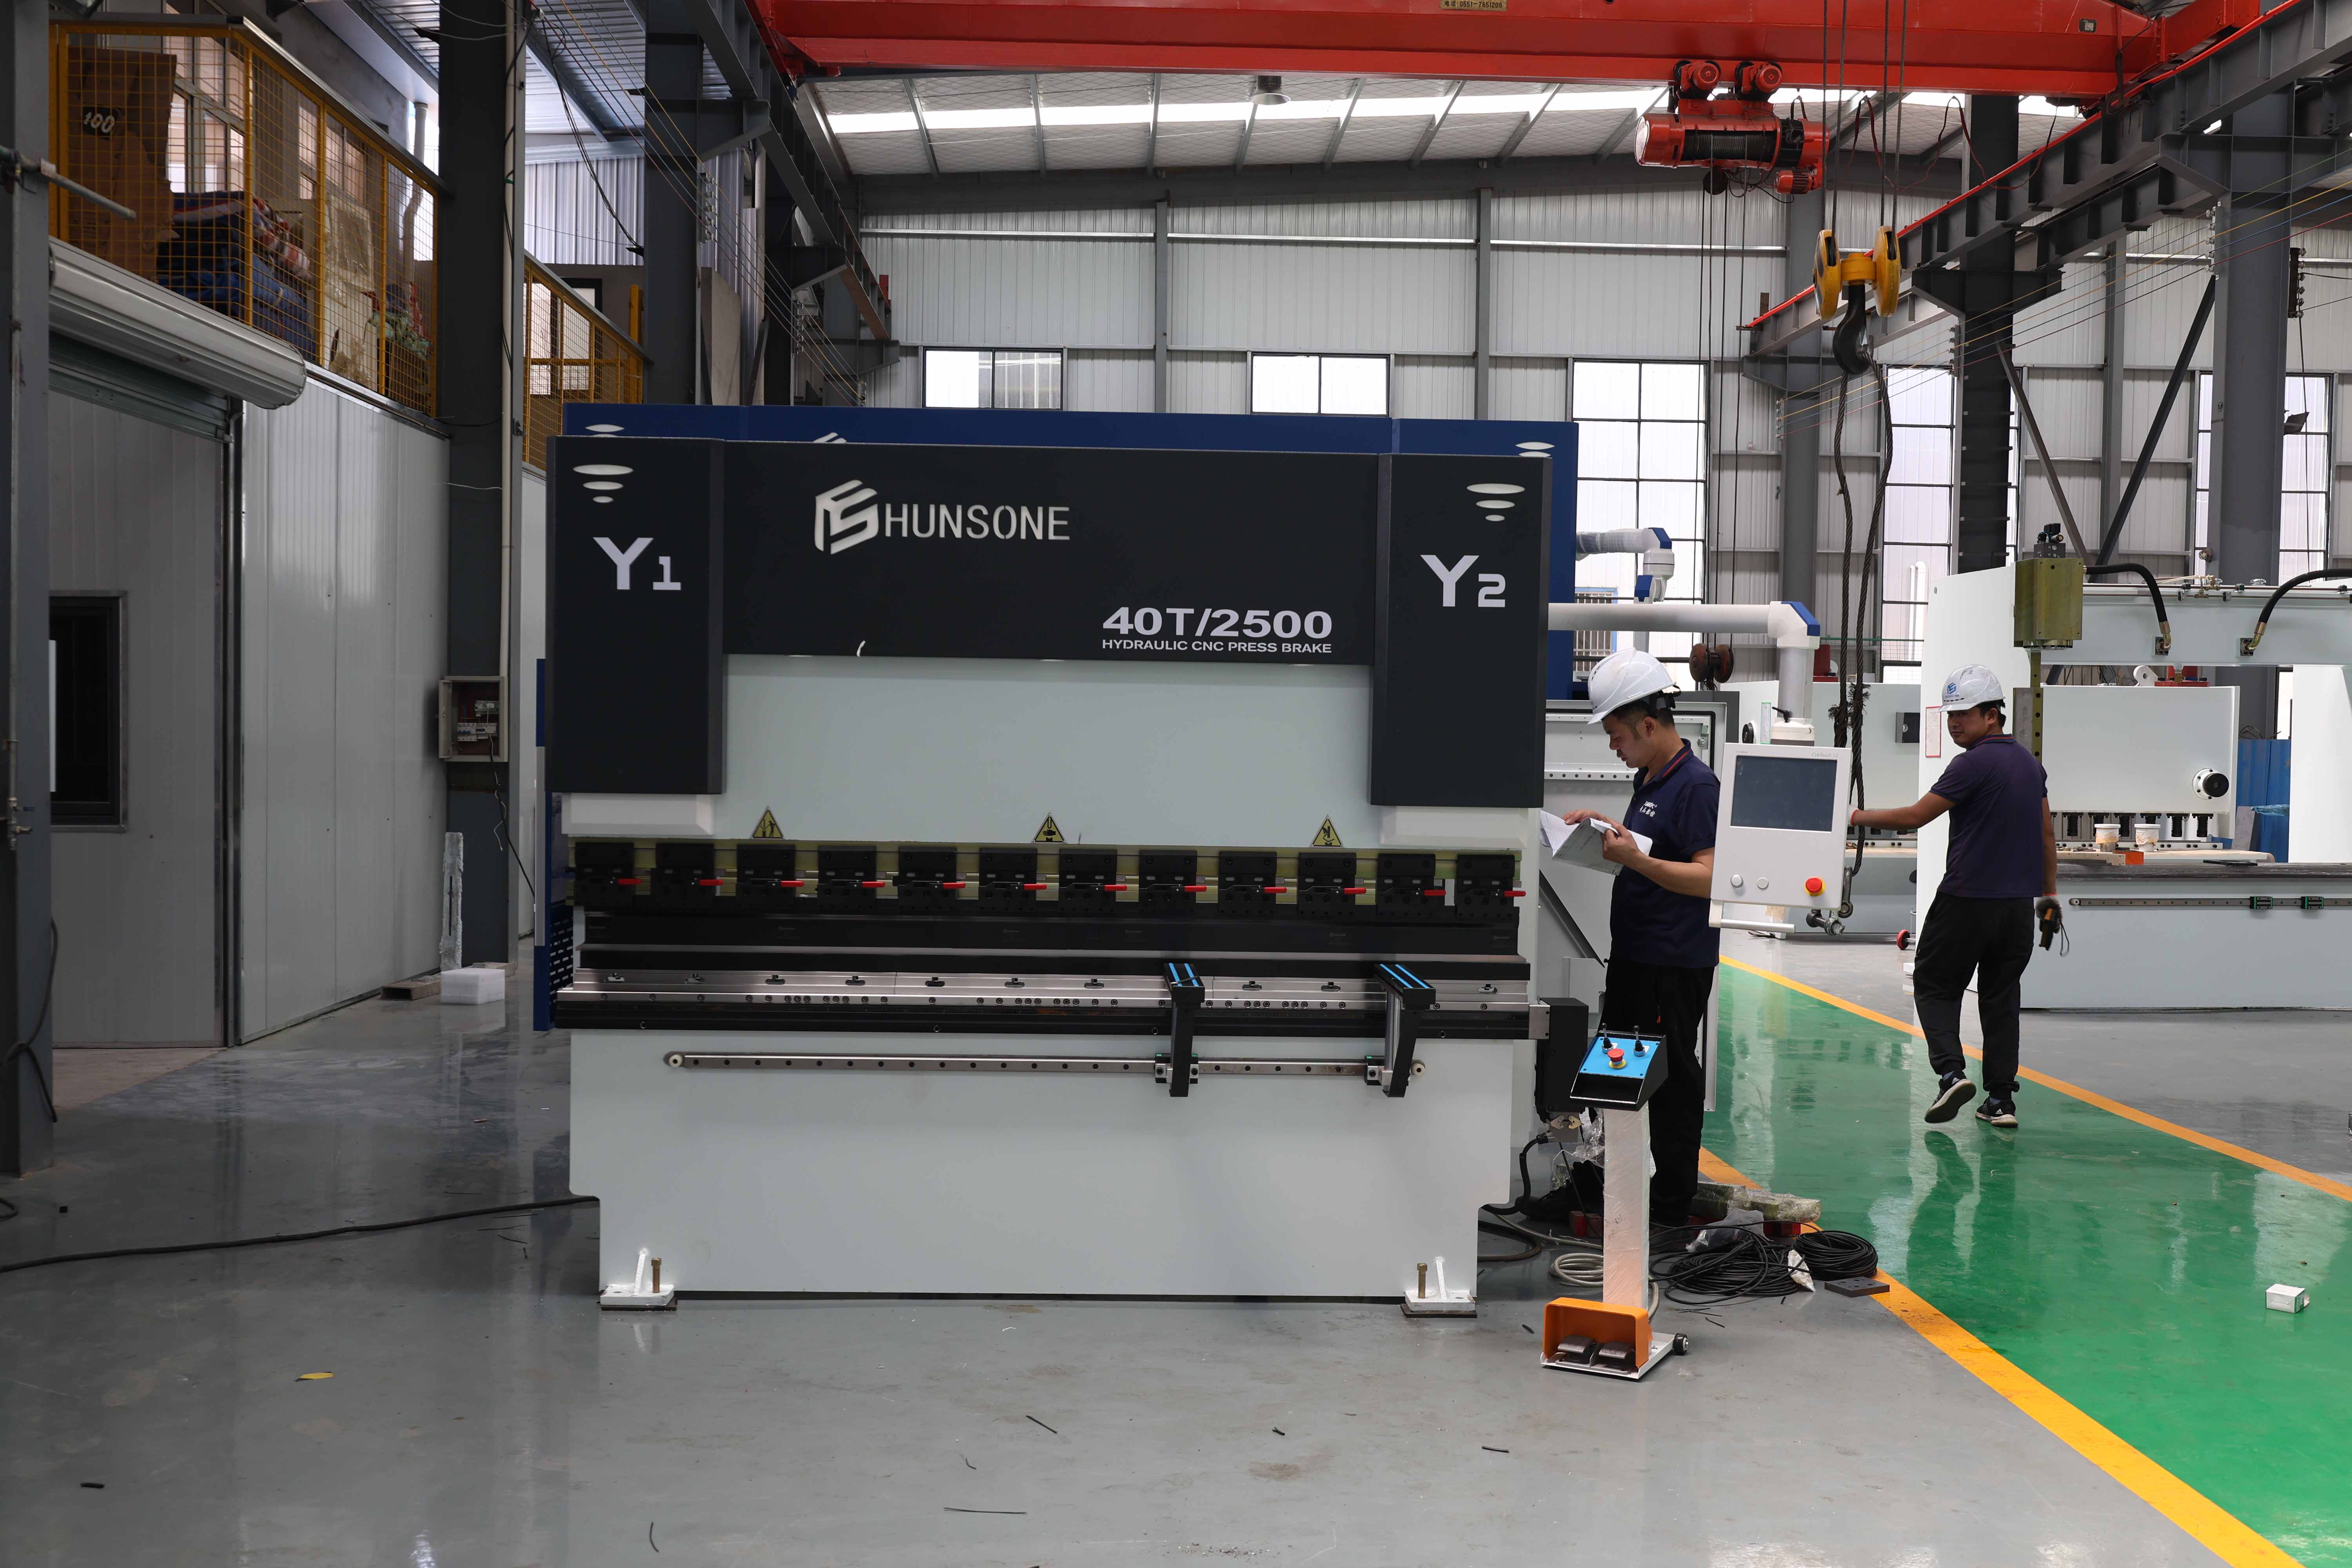
A spec sheet can rattle off wheelbase, head tube angle, and bottom bracket drop, but those numbers rarely capture how a frame actually behaves beneath you. The way a downtube tapers near the bottom bracket, the subtle curve of a seatstay, the weld quality at the head tube junction—these details whisper about ride quality, stiffness, and compliance long before your first pedal stroke. Look closely at the dropouts: are they forged or stamped? That single choice often reveals more about durability and alignment than any geometry chart.
Paint depth, cable routing, and even the placement of bottle bosses hint at the designer's priorities. A frame with internal routing that rattles on rough gravel tells you the brand chased aesthetics over function. A raw titanium finish with perfectly brushed welds suggests a builder who trusts the material rather than hiding it under thick coats. Run your fingers along the chainstay yoke—if it's asymmetrical or heavily machined, you're likely looking at a frame engineered for real-world flex patterns, not just static lab tests.
Next time you're in a shop, ignore the marketing poster and pick the frame up. Feel the weight distribution, inspect the bottom bracket shell thickness, check if the seat tube is butted or straight gauge. Those tactile clues—the things no PDF can communicate—will tell you whether that frame deserves your hard-earned miles or just looks good on a website.
A Control Panel Your Operators Won't Dread
Most control panels fail before a single button is pressed. They bury critical readings under layers of menus, scatter alarms with identical tones, and demand that operators memorize color codes that change from one shift to the next. This panel starts from a different question: what does the person standing in front of it actually need to see right now? The answer shapes every layout decision, from the size of the stop button to the spacing between gauges.
Instead of cramming every possible data point onto one screen, we group controls by task sequence. Start-up checks live on the left. Normal running adjustments sit in the center. Emergency actions are never more than one reach away. Labels use plain verbs, not engineering shorthand, so a new operator can follow the flow without a manual. And when something does go wrong, the panel tells you what happened, where, and what to do next - in that order, without a wall of blinking lights.
The result is a panel that feels less like a test and more like a tool. Operators stop dreading the next alarm because they know the panel won't punish them with ambiguity. They trust it, and that trust shows up in faster responses and fewer mistakes. That's the whole point.
Tooling Changeover Turns Minutes Into Money
At a stamping plant in Ohio, a press sat idle for 47 minutes every time operators swapped out a die set. Three changeovers per shift meant over two hours of lost production daily. At 40 parts per minute and a margin of $0.18 per part, that idle time quietly erased roughly $1,000 every single day. Nobody noticed because the loss was spread across the month, hidden inside routine downtime reports. But the math was brutal: every minute of tooling changeover was a minute the machine wasn’t printing money.
The fix wasn’t a new press or a bigger maintenance budget. It was rethinking the changeover itself. Bolts were replaced with quick-release clamps, tool carts were pre-staged within arm’s reach, and a simple shadow board eliminated the hunt for wrenches. Within three weeks, the average changeover dropped from 47 minutes to 9. The same press, same operators, same product—but now an extra 114 minutes of production per shift. That added up to 41,000 additional parts a week, flowing straight to the bottom line without hiring a single person or buying a single machine.
What gets measured gets managed, but what gets converted into cash gets funded. When maintenance teams treat tooling changeover as a revenue leak instead of a routine chore, priorities shift. A 5-minute reduction might sound trivial until you multiply it by 200 changeovers a month. That’s 1,000 minutes—nearly 17 hours—returned to production. For most factories, that’s the difference between meeting a quarterly target and missing it. The minutes were always there. They were just waiting for someone to turn them into money.
What to Ask About Service Before the Sale Ends
Before the promo window closes, get specific about what the service contract actually covers. Ask whether wear-and-tear items like brake pads, wipers, and fluid top-offs fall under the plan or count as extras. A lower upfront price often hides a narrower scope, so have the dealer mark exactly which components and labor hours are included.
Time is another detail that gets glossed over in the final push. Find out the average turnaround for common repairs, whether a loaner car or shuttle is guaranteed, and how far ahead you need to book. If the service center is third-party rather than manufacturer-run, confirm they have certified techs for your exact model and year, otherwise the discount won't matter much when you're waiting two weeks for a diagnostic.
Also ask what happens to the service package if you sell or trade the vehicle before the contract ends, and whether there are cancellation or transfer fees buried in the fine print. Nail down the small stuff now: diagnostic charges, shop supply fees, and disposal costs can each eat into the savings you're trying to lock in.
The Costs That Don't Show Up on the Invoice
Most businesses treat an invoice as the final word on what a project or purchase actually costs. That assumption falls apart the moment something small goes wrong. A supplier ships the wrong part, a contractor arrives two days late, a piece of equipment needs an unplanned calibration. None of those line items appear on the bill, but they quietly consume payroll hours, delay dependent work, and force managers to reshuffle schedules that were already tight.
Then there are the costs baked into internal routines. Every time someone has to rekey data from a vendor portal into an internal spreadsheet, reconcile a discrepancy, or chase down a missing approval, the meter runs. Those minutes rarely get tracked against a specific invoice, so they vanish into overhead. Over the course of a quarter, a team can lose hundreds of hours to follow-ups, corrections, and workarounds that exist only because two systems do not talk to each other.
Some hidden costs are even harder to see because they show up as wear on people rather than budget lines. Rework caused by vague specifications, meetings held to resolve preventable errors, and the mental switching cost of juggling half a dozen vendor portals all drain attention. A leader who looks only at the invoice sees a fair price. A leader who looks at the total effort sees a much more expensive story.
FAQ
Look beyond tonnage and bed length. For precision work, focus on ram repeatability, frame deflection characteristics, and the quality of the CNC backgauge. A vendor that can provide measured deflection data and demonstrate consistent angle control across multiple test bends is worth more than one that only lists nominal specs. Ask for a live bending trial with your own material and thickness range.
Request a detailed capability study that includes actual bend angle variation, not just a brochure figure. Have the vendor run a series of test pieces in your material, then check angular consistency and dimensional repeatability with your own inspection equipment. Ask about thermal compensation and how the machine maintains accuracy during long production runs.
The controller directly affects setup time, error recovery, and programming complexity. Evaluate the interface by having your operators use it during a demonstration. Look for features like automatic bend sequence calculation, collision detection, and offline programming compatibility with your CAD software. A vendor with a closed or difficult-to-learn control can create a hidden labor cost.
It can determine long-term flexibility. Check if the machine accepts standard tooling styles or locks you into a proprietary clamping and punch/die system. Proprietary systems can offer faster changeovers but limit your ability to source alternative tooling. Ask to see how existing tooling inventory can be adapted and whether the vendor's tooling supports the precision profiles you commonly bend.
Prioritize response time for critical failures over broad warranty language. Ask for local service technician availability, typical spare parts lead times, and remote diagnostics capability. Request references from shops with similar precision requirements and ask them about downtime after installation and how the vendor handled calibration drift or software bugs.
These include excessive tooling replacement due to poor alignment, frequent recalibration, operator frustration from unintuitive controls, and production bottlenecks when service is delayed. In precision fabrication, a slightly cheaper machine that drifts out of tolerance can create scrap and rework that quickly erases the upfront savings.
Don't rely only on a factory demo with ideal material. Bring your own sheet metal stocks, including the hardest and thinnest gauges you process. Run multiple bending sequences and measure angle consistency at different positions along the bed. Ask the vendor to leave the machine on for several hours and then repeat the test to reveal thermal drift.
A good vendor asks about your specific tolerance requirements, material variations, and downstream processes before recommending a model. They offer a documented repeatability test and are transparent about how frame design, crowning, and angle measurement work together. Average vendors lead with tonnage and price; precision-focused vendors lead with process capability and validation.
Conclusion
Precision fabrication hinges on more than advertised accuracy: the real question is whether a press brake can hold your required bend tolerance through an entire shift, not just during a demo. A rigid, well-built frame matters because it resists deflection under load, and you can feel that difference in the machine's stance long before you read a spec sheet. Equally telling is the control panel—if your operators hesitate to touch it, throughput suffers. Look for interfaces that reduce setup guesswork and store repeat jobs, because every minute spent deciphering menus is a minute not bending metal.
Tooling changeover is where profit quietly leaks: a vendor who offers quick-release clamping and offline setup stations turns ten-minute die changes into two, compounding across hundreds of orders. Before the sale ends, pin down service response times, spare parts availability, and whether technicians are local or flown in—downtime costs more than any payment plan. Finally, count the hidden invoice lines: freight, rigging, training, software licenses, and even floor reinforcement. A cheap machine that demands a new foundation or a week of operator frustration is no bargain. Choose the vendor who understands your parts, your tolerances, and your floor, not the one with the glossiest brochure.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/