China Sandpaper Jumbo Roll: A Practical Guide to Choosing and Using Abrasive Rolls
2026-09-14
If you've ever wrestled with a sandpaper jumbo roll that clogs or tears mid-run, you already know the cost of downtime. The difference between a smooth operation and a bottleneck often comes down to details most buyers overlook: backing weight, bond strength, and roll consistency. This guide cuts through the noise with real-world advice from SHENZHEN SUN ABRASIVES, a manufacturer that specializes in abrasive rolls built for demanding jobs.
Reading a Jumbo Roll Spec Sheet Without Glazing Over
Jumbo roll spec sheets hit you with a wall of numbers—basis weight, caliper, moisture, tensile strength—and it’s tempting to just nod and skip to the diameter. But glazing over means missing the details that decide whether that roll runs clean or jams your converting line. Start by zeroing in on the two specs that actually change roll behavior day to day: basis weight and moisture. A 45-pound sheet with 8% moisture handles completely differently than the same weight at 6.5%. If you don’t check both against your machine’s sweet spot, you’ll chase wrinkles for a week.
Next, look at the roll’s construction notes buried in the fine print. Core size, winding tension, and splice count rarely make the headline numbers, but they determine how the roll unwinds. Too much tension near the core gives you star-shaped defects; too little lets the outer layers telescope in transit. A spec sheet that only lists “standard winding” is basically saying “good luck.” Ask for the actual tension profile or at least the unwind stand compatibility—one line of data can save you three hours of downtime.
Finally, don’t read a jumbo roll spec sheet in isolation. Compare it to the last three rolls from the same mill. Even if every number falls within the printed tolerance, a gradual creep in caliper or a dip in tear strength tells you the paper machine is drifting. That trend matters more than any single measurement. When you spot a spec drifting toward the edge of the acceptable range, that’s your cue to call the supplier before the roll gets on a truck—not after it’s already unwinding into your floor.
Grit Selection for the Work You Actually Do
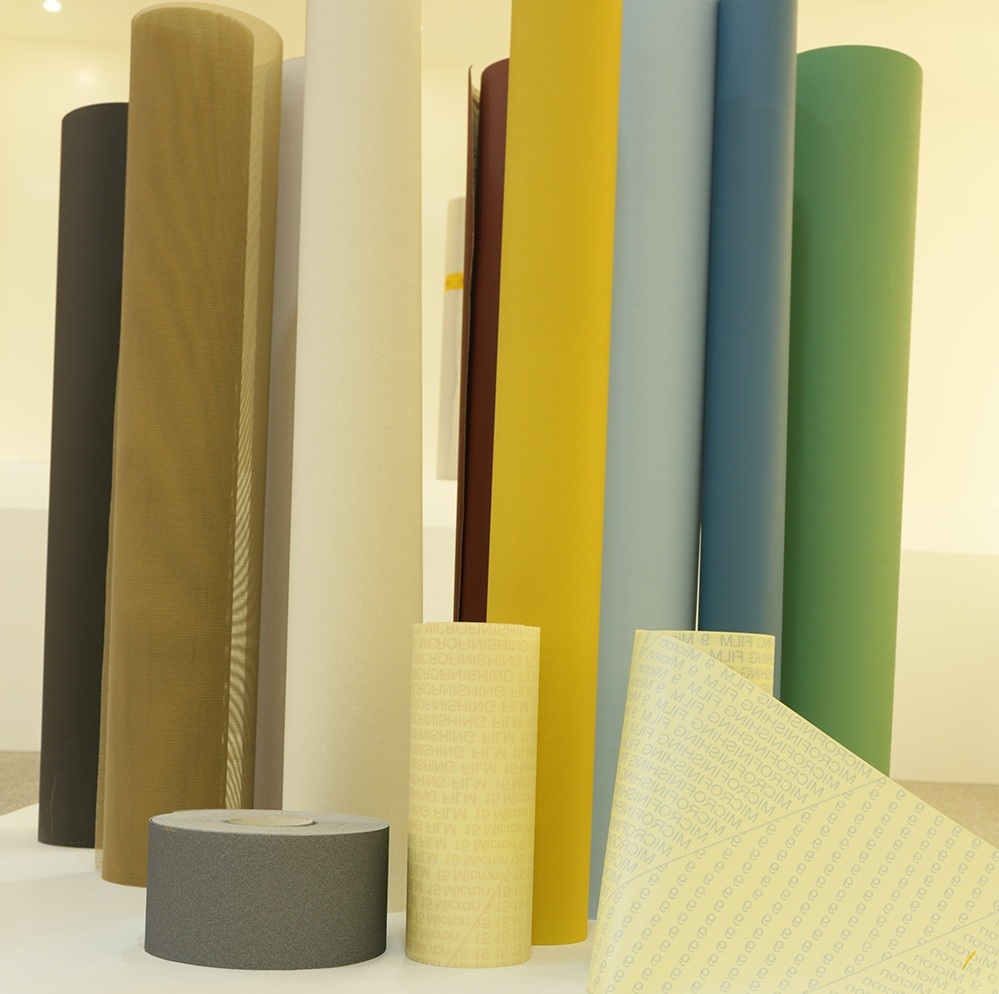
Matching grit to the task often gets reduced to picking a single number off a chart, but that approach ignores how different materials actually fail under real working conditions. The grit that cuts soft wood quickly will smear aluminum or glaze over hardened steel. Instead of chasing a universal recommendation, look at what the surface tells you after a few passes: if the abrasive loads up and stops cutting, drop down a grit or switch to a ceramic blend; if the finish feels rough even after light pressure, step up gradually rather than jumping three grades at once.
The shape and backing of the abrasive matter just as much as the grit number once you move beyond flat, open areas. Tight corners, weld seams, and contoured profiles can make a nominally coarse grit act fine, or force a fine grit to dig in too aggressively because the contact patch shrinks. Pay attention to how the tool behaves in those transitions—if you find yourself tilting the disc to reach a fillet, you are no longer using the grit the way it was designed, so compensate with a lighter touch or a more flexible backing rather than changing the grit alone.
A practical way to settle on a range is to keep two or three grits within arm's reach for the same job and let the actual material dictate the progression. Start with the coarsest option only where you need to remove stock quickly, then move up as soon as the scratches become the dominant feature you see. The best grit choice is the one that lets you stop sanding sooner, not the one that promises the lowest number on a spec sheet.
Backing Material: Cloth, Paper, or Film?
Cloth backings bring a level of toughness that paper simply can't match on aggressive work. A cotton or polyester cloth base absorbs the punishment of curved surfaces and high-pressure grinding without cracking or delaminating, which is why it shows up in heavy sanding belts and discs. Paper, on the other hand, wins on price and precision for lighter tasks—its stiffer surface creates an even scratch pattern for paint prep and fine wood finishing, but it gives up quickly under repeated flexing or moisture. Film sits between them, offering a smoother, more consistent base than paper with tear resistance close to cloth, and it really proves its worth in wet sanding or fine automotive work where a uniform backing translates directly to a uniform finish.
Choosing the right backing often comes down to how much abuse the material will take and how consistent the surface needs to be. If the job involves heavy pressure or odd angles, cloth is the safe bet. For flat, delicate finishing on a budget, paper is hard to beat. Film is the specialist's choice, especially when water or solvents are involved and the final surface quality leaves no room for backing irregularities.
Mounting Wide Rolls Without Wasting Inches
Loading a wide roll often comes down to one overlooked habit: aligning the core before you lift. Instead of eyeballing the position once the roll is already on the spindle, slide the core against the fixed flange first and lock it before introducing the media. This tiny sequence change keeps the leading edge square from the start, so you aren't trimming away a few inches just to correct a skew.
If your machine has adjustable side guides, use them as a physical reference rather than a suggestion. Bring both guides snug to the roll edges after the core is centered, then walk to the front and check that the media path is parallel to the platen. A quick visual check here prevents the slow drift that turns into a wrinkled or uneven cut after only a few feet of travel.
Finally, give yourself a small buffer at the leading edge but not a sacrificial strip every time. Pull the media forward only far enough to clear the pinch rollers or cutter, then set your origin. Most of the "waste" on wide rolls isn't from the material itself; it's from starting the job before the roll has settled into its natural alignment.
Keeping Abrasive Rolls Sharp Longer on the Line
The real enemy of abrasive roll sharpness isn't the metal you're grinding—it's the loading that builds up between the grains. When dust and swarf pack into the open spaces, the abrasive can't bite and the roll starts to skate instead of cut. A quick pass with a stiff brush or a low-pressure air blast every few cycles does more for edge retention than most people expect. It's cheap, takes less than a minute, and brings back that crisp cutting feel without changing the roll.
Tension and line speed get overlooked because they're set once and forgotten. But running a roll too tight fractures the grains early, while too little tension lets the belt slip and glaze from heat. Dropping the line speed by even five to ten percent lowers the temperature at the contact point enough to keep the resin bond from softening. One operator I know kept a log and found that a slight speed reduction stretched roll life from two shifts to almost three with no measurable drop in finish quality.
Storage and handling between runs are just as important as what happens on the machine. Rolls left near a heat source or in a damp corner will either sweat or become brittle before you ever mount them. Rotate stock so older rolls get used first, and if the line stops for more than a few minutes, back the contact wheel away so the abrasive isn't sitting under pressure. That small habit prevents flat spots and heat damage that show up as premature dulling on the next start-up.
When a Roll Is Done: Fraying, Loading, and Other Telltales
The first hint that a roll is nearing its end often comes from the edges. You might notice fine threads peeling away from the sides, a kind of fraying that happens when the outermost layers have been wound too tightly or exposed to repeated friction. This fraying isn't just cosmetic; it signals that the remaining material may be thinner or more fragile than the first part of the roll.
Another telltale is what many call loading. As the roll unwinds, the tension changes, and you can feel a slight resistance or hear a subtle creaking from the core. Sometimes the roll starts to wobble on its spindle because the inner layers have shifted. If you pay attention to these small shifts, you can swap in a fresh roll before the old one snaps or tears at an inconvenient moment.
Beyond fraying and loading, other signs include uneven winding patterns, a visible change in the roll's diameter, or even a faint papery smell when the core gets exposed. Each roll behaves a little differently depending on how it was stored and handled, but once you learn to read these cues, you'll rarely be caught off guard.
FAQ
A jumbo roll is essentially a large master roll of abrasive material—often over a meter wide and hundreds of meters long—that can be cut down into belts, sheets, discs, or custom strips. Unlike pre-cut sheets, it gives you the freedom to produce any size you need, which is especially useful in woodworking or metal shops that run multiple tools and odd-shaped sanding blocks.
Think about the task rather than the grit number. For heavy material removal or stripping old paint, start around 40 to 60 grit. For general surfacing before finishing, 80 to 120 grit hits the sweet spot. If you're sanding between coats of finish, go 180 to 240 or finer. Many Chinese manufacturers use the same FEPA or ANSI grading, but it's always smart to test a small piece first, especially if the price seems unusually low.
The backing is the real deciding factor. Paper backing—typically A, C, or E weight—is lighter and more flexible, good for hand sanding or fine work. Cloth backing, often cotton or polyester blends, resists tearing and handles machine sanding or contoured surfaces much better. Film backing shows up in finer grits and gives a very uniform finish. For most general shop use, a C-weight paper or light cloth roll covers both worlds.
Lower cost usually comes down to production scale, labor costs, and raw material sourcing rather than automatically meaning poor quality. That said, consistency can vary more from batch to batch, so your first order should be a trial run. Check for even grit distribution, backing strength, and whether the adhesive holds up under heat. A reliable supplier will tell you the exact abrasive type—aluminum oxide, silicon carbide, or zirconia—and won't dodge questions about re-coating or open-coat vs. closed-coat.
Yes, but how you cut matters. Use a sharp utility knife or heavy-duty scissors, and score the backing first on cloth rolls to avoid frayed edges. A straightedge and a cutting mat help keep strips square. If you're making belts, you'll need proper skiving and splicing equipment, because a butt joint with ordinary tape won't survive the drum heat. For sheets and discs, punched or laser-cut shapes from the same jumbo roll tend to hold their edge better than hand-cut circles.
Letting the roll sit flat on a concrete floor or near an open window. Moisture can curl paper backing, weaken the bond between abrasive grains and backing, and cause the roll to telescope when you unwind it. Store it vertically in a dry area, ideally in the original plastic sleeve or a sealed tube. If the roll does get damp, unroll a few meters and let it acclimate slowly instead of forcing it flat.
The main concern isn't the origin but the material you're sanding and the abrasive type. Silicon carbide and zirconia produce fine dust, so a dust mask or respirator is a must. If you're sanding metal, watch for sparks and keep the work area clear of flammable dust. Also, some cheaper rolls may shed more grit early on, so wipe down the surface and check for loose abrasive before applying a finish.
Don't judge by the first meter. Track how long a roll lasts on a typical job, how evenly it wears, and whether you're getting consistent scratch patterns. If you find yourself changing strips twice as often, the 'savings' evaporate quickly. A good test is to sand a painted board with a fresh strip and compare the number of passes before the paper clogs versus a brand you already trust.
Conclusion
Working with China jumbo sandpaper rolls starts with reading the spec sheet like a floor supervisor, not a data clerk. Don't glaze over the abrasive type, grit range, backing weight, and roll width — those four numbers decide whether you're fighting the line or feeding it. Match grit to the job you actually run: 40-80 for heavy stock removal or weld blending, 120-180 for finish sanding before coating, and 220+ only when the surface truly needs a polish. Backing matters just as much as grit. Cloth handles edge work and contoured parts without tearing, paper gives you a flatter, cheaper cut on flat panels, and film is worth the extra cost when you need consistent scratch depth on high-end finishes. Don't buy a jumbo roll just because the price per square meter looks good if the backing will shred on your first shift.
Mounting wide rolls without wasting inches means measuring your machine's true cutting width, not the nominal roll width, and using a slitter that leaves clean, square edges. When you run a roll, keep it sharp by adjusting pressure and speed instead of forcing a dull belt to bite harder — that just loads the abrasive and burns the workpiece. Watch for the telltales: frayed edges mean your tracking is off or the roll is too wide for the guides; loading shows you're using too fine a grit or too much heat; and a shiny, glazed surface means the abrasive is spent, even if you can still see grit. Pull the roll when those signs stack up, because running a dead roll longer only costs you in rework and operator frustration. A jumbo roll isn't cheap, but it pays for itself when you treat it like a tool, not a consumable to squeeze dry.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn